
Bottled water production: solve one problem
How to Diagnose Loose, Torn or Skewed Water Bottle Shrink Packs
A weak finished pack may originate before the tunnel. Follow the bottles and film through the process so a heat adjustment does not hide a grouping, material or sealing problem.
Keep the bottle, film lot and pack pattern fixed. Locate the first defective stage: group formation, film application, seal, tunnel exit or discharge. Compare an approved sample with the failed pack before requesting equipment changes.
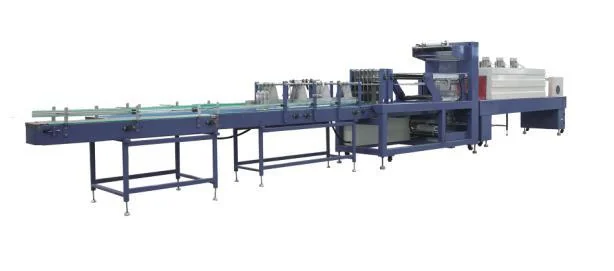
Define the defect and the finished-pack requirement
Describe loose film, seal opening, film splitting, distorted bottles or a skewed group separately. Photograph the approved pack and failed pack with the seam, leading edge and travel direction visible. Record whether damage starts before the tunnel or during handling.
Illustrative continuous rate: 12,000 bottles/hour requires 33.33 six-bottle packs/minute or 16.67 twelve-bottle packs/minute before losses. Confirm packs per cycle and orientation. A cycle/minute figure cannot be compared directly with bottles/hour.
Follow the first visible defect
These observations narrow an investigation; they do not diagnose a component without a controlled test. A torn pack can involve several causes, including an incorrect film specification or damage during transfer.
| First defect | Record or compare | Responsible scope |
|---|---|---|
| Group already skewed at film entry | Bottle dimensions, grouping count, guide position and transfer timing | Grouping and infeed |
| Film wrinkles or registration changes before sealing | Film specification and lot, roll direction, tracking and cut position | Material and film feed |
| Seal opens before a sound pack reaches discharge | Seam position and approved material-specific sealing record | Film joint and sealing system |
| Pack leaves the tunnel sound but loosens or tears later | Cooling time, discharge transfer and actual handling condition | Cooling, conveying and distribution test |
Change one factor and retest the complete pack
There is no universal tunnel temperature or film thickness for all water packs. Do not open guards, touch hot equipment or change heating from this article. Obtain approved material and machine instructions.
- 01
Hold bottle revision, film lot, fill condition and pack arrangement constant.
- 02
Mark the travel direction and inspect samples at each accessible approved observation point.
- 03
Have a qualified technician compare film feed, sealing and tunnel records with supplier-approved settings.
- 04
Change one documented factor and count accepted packs and rejects over the same interval.
- 05
Check the pack after cooling and representative handling, not just when it looks tight at the tunnel exit.
Prepare a useful packing-equipment or service request
Ask for an accepted finished pack at the required rate, including orientation, cooling and downstream handling. If the existing grouping or seal system cannot meet the format, define that module explicitly. A new tunnel alone does not correct a proven infeed problem.
- Bottle drawing, filled mass, pack pattern and finished-pack dimensions.
- Film type, specification, lot and supplier process window.
- Approved and failed pack photographs with seam and travel direction.
- Location and frequency of first defect, plus start/restart behavior.
- Accepted packs/minute, bottles/pack and actual packs/cycle.
- Cooling, discharge, pallet handling and proposed acceptance test.
Questions buyers ask
Should I raise tunnel temperature when packs are loose?
First locate where the defect starts. Grouping, film fit, sealing and post-tunnel handling can produce similar symptoms. Use a material-specific approved process window for any technician-led heat adjustment.
Does a 3×4 pattern work the same as 4×3?
Both contain twelve bottles, but orientation relative to travel changes width, length, film and grouping conditions. Approve the actual direction and sample; equal bottle count does not establish compatibility.
Related troubleshooting guides
Water filling machine low output
Water filling machine low output →Cap leaks after capping
Cap leaks after capping →Wrinkled or skewed bottle labels
Wrinkled or skewed bottle labels →Ask Allot Tech to review the evidence
Send your machine identification, package drawing and timed observations. State what is unknown so the proposed scope follows the actual problem.