
Buyer scenario · Brownfield machinery
Replace or Add One Machine Without Breaking the Existing Line
A replacement is an interface project. The new machine must accept the real upstream product, deliver the real downstream product and fit the installed space, elevation, controls, utilities, operator access and maintenance route.
DIRECT ANSWER
What the buyer should decide
Record the existing line before selecting the replacement. Photos help, but dimensioned drawings, nameplates, bottle and pack samples, signal information and operating behavior provide a stronger basis.
| Decision field | Confirm | Why it changes the purchase |
|---|---|---|
| Physical fit | Footprint, height, maintenance and rigging path | Prevents a machine that cannot be installed or serviced |
| Product transfer | Infeed/outfeed elevation, direction, speed and stability | Controls jams and transition rework |
| Control fit | Signals, safety chain, PLC/network and stop behavior | Defines integration work before shipment |
BUYER DECISION WORKBENCH
Match the replacement scope to the machine being changed
Keep the existing line as the reference and quote the connecting work with the new machine. Replacing a labeler, filler or packer changes different interfaces; using one generic installation allowance hides those differences.
| Replacement | Retained interfaces to measure | Common additional scope |
|---|---|---|
| Rinsing/filling/capping monoblock | Bottle infeed, discharge, cap delivery, water/cleaning circuits and line-state signals | Transfer parts, cap-feed changes, piping connections, format parts and coordinated commissioning |
| Labeler or coder | Wet/dry bottle condition, spacing, orientation, code location and reject handling | Drying or metering, guides, inspection, recipe handoff and applicator-specific services |
| Shrink wrapper or case packer | Bottle-equivalent demand, lanes, grouping, pack exit and pallet handling | Infeed/dividing conveyors, pack change parts and downstream transfer |
| Bottle blower | Approved preforms, molds, air/cooling and filler connection | Utility capacity, discharge transfer, demand/stop signals and bottle-quality trials |
BUYER DECISION WORKBENCH
Plan the change around a defined production stop
Prepare the measurements, parts and agreed tests before the production stop. The permitted shutdown window belongs in the scope, but no installation duration is assumed from a machinery photograph.
| Stage | Prepare or complete | Release condition |
|---|---|---|
| Before shutdown | Agree drawings, adapters, utility connections, signal ownership, samples and test materials | The installation team has a controlled scope and a rollback decision. |
| During the agreed stop | Isolate equipment under the site's approved procedure and install the agreed change | Qualified personnel complete mechanical, electrical and safety verification. |
| Before production release | Trial every approved format, check line states, rejects, codes and pack transfer | Record good-output results, exceptions, operator handover and remaining actions. |
This is a planning sequence, not instructions for working on energized machinery. Site safety and machine procedures govern installation and testing.
REQUIRED INPUTS
Prepare the evidence before selection
Missing fields should remain marked as open rather than converted into assumptions.
- Existing layout and dimensions
- Machine nameplates and manuals
- Bottle/pack samples
- Measured production issue
- Signal and utility information
- Available shutdown and installation window
TRADE-OFFS
Make the choice visible
Every option changes the machinery, operating work or project boundary.
Like-for-like fit
Simplifies interfaces but may preserve the original constraint.
Higher machine rating
Adds no value when adjacent machines or utilities remain limiting.
Custom transition work
May solve a difficult boundary but increases site verification and FAT needs.
PURCHASING RISKS
Do not let these gaps hide in the quotation
Carry every unresolved item into clarification and contract documents.
- Quoting from photos alone
- Assuming matching BPH means matching transfer
- Ignoring old control documentation
- Forgetting rigging, access and production downtime
WORK SEQUENCE
Move from data to a controlled next action
- 01
Measure the installed line.
- 02
Define the present constraint.
- 03
Record every interface.
- 04
Review options and site work.
- 05
FAT the machine and simulated interfaces.
- 06
Close the site installation plan.
Representative machinery views
Compare the machinery form before selecting the project scope
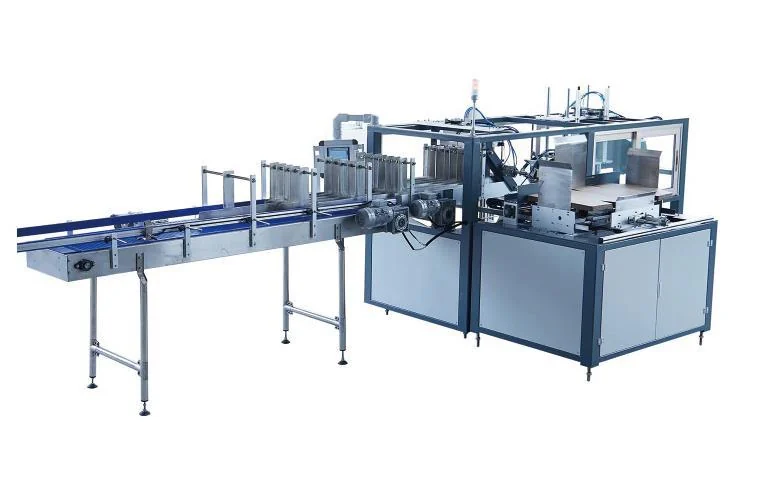
Technical descriptions are selection guidance. Final machine, capacity, material, component, interface, utility and service details must be confirmed in the project proposal.
Content reviewed:
NEXT PURCHASING ACTION
Document the installed boundary first.
Send drawings, elevations, bottle data, controls and the problem the new machine must solve.