
Buyer scenario · Output improvement
Upgrade the Bottleneck the Line Actually Has
An output problem may come from a slower machine, frequent small stops, poor accumulation, format setup, package material, utilities or operator recovery. Replacing the apparent slowest machine without production evidence can move the bottleneck instead of improving saleable output.
DIRECT ANSWER
What the buyer should decide
Collect time-based production evidence and separate planned changeover, equipment fault, upstream starvation, downstream blocking, reject loss and utility interruption. Use rated speeds as reference inputs, not as the diagnosis.
| Decision field | Confirm | Why it changes the purchase |
|---|---|---|
| Speed constraint | Which machine has the lowest effective speed on the same format? | Identifies a possible sustained bottleneck |
| Stop constraint | Which repeated event removes the most saleable time? | May favor reliability or interface work over replacement |
| Flow constraint | Where does product starve, block or accumulate poorly? | May favor conveyors, sensors or control changes |
BUYER DECISION WORKBENCH
Choose the upgrade from the loss pattern
A speed increase helps only when that machine is the sustained constraint. First compare the same bottle, pack and observation window; distinguish failures from material replenishment and deliberate format changes.
| Observed loss | First improvement route | Equipment to consider if the cause is confirmed |
|---|---|---|
| Filler repeatedly blocked by packing | Compare packer output and material-change stops with filler discharge | Packing capacity, material feed or a justified short-stop buffer |
| Filler repeatedly waiting for empty bottles | Compare blower or bottle-loading output and transfer interruptions | Bottle handling, preform feed, blower or transfer changes |
| Packing starved while filler has local faults | Restore the filler condition and investigate repeat faults | A scoped filler repair or replacement when condition warrants it |
| Losses clustered around size changes | Map parts changes, adjustments and first-off release time | Format parts, repeatable adjustments and recipe support |
| Adequate speed but frequent utility faults | Review measured supply under simultaneous demand | The constrained air, cooling, water or electrical service |
BUYER DECISION WORKBENCH
A faster filler cannot remove a slower packing constraint
Illustrative steady-flow example: the filler is capable of 10,000 bottles/hour on the test format, while the packer accepts only 8,000 bottle-equivalents/hour. Losses and buffers are omitted here to isolate the sustained-rate constraint.
| Change | Upstream rate | Downstream limit | Steady-flow implication |
|---|---|---|---|
| Current pair | 10,000 bottles/hour | 8,000 bottle-equivalents/hour | Packed throughput is bounded by the 8,000 downstream rate. |
| Filler-only upgrade | 12,000 bottles/hour | 8,000 bottle-equivalents/hour | The downstream limit remains 8,000; more filler capacity alone does not remove it. |
| Downstream upgrade to review | 10,000 bottles/hour | 12,000 bottle-equivalents/hour | The filler becomes the lower rated stage; actual good output still includes operating losses. |
Extra conveyor can absorb a brief interruption, but it cannot absorb a continuous production-rate mismatch indefinitely. A real upgrade review must include measured stops, material behavior, control states and safe operating limits.
REQUIRED INPUTS
Prepare the evidence before selection
Missing fields should remain marked as open rather than converted into assumptions.
- Machine rated speeds
- Actual output by SKU and shift
- Stop and reject observations
- Changeover records
- Utility pressure/temperature interruptions
- Layout and control behavior
TRADE-OFFS
Make the choice visible
Every option changes the machinery, operating work or project boundary.
Replace versus stabilize
Maintenance or controls may recover more output than a new machine.
More accumulation
Buffers can decouple short stops but may consume space or damage product.
Higher rating
Requires adjacent machines, utilities and pack handling to accept the new flow.
PURCHASING RISKS
Do not let these gaps hide in the quotation
Carry every unresolved item into clarification and contract documents.
- Using one good shift as the baseline
- Ignoring reject and rework losses
- Changing a machine without the signal matrix
- Forecasting output from nameplate speed alone
WORK SEQUENCE
Move from data to a controlled next action
- 01
Collect the current-state evidence.
- 02
Normalize machines to one SKU.
- 03
Identify speed, stop and flow constraints.
- 04
Model the interface after the proposed change.
- 05
Define FAT and site acceptance evidence.
Representative machinery views
Compare the machinery form before selecting the project scope
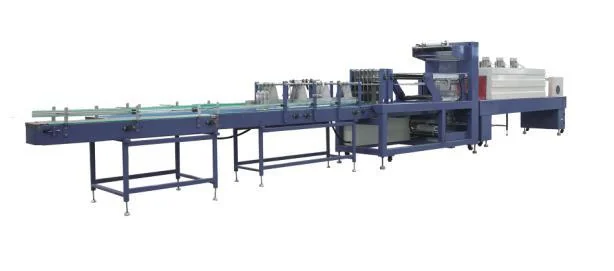
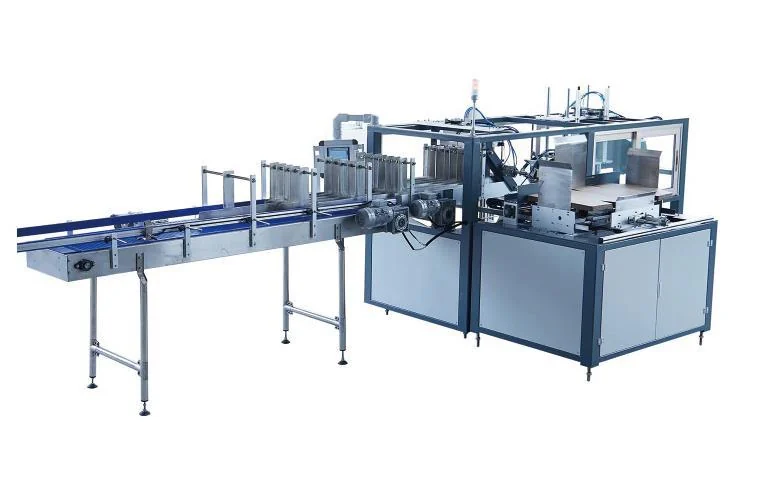
Technical descriptions are selection guidance. Final machine, capacity, material, component, interface, utility and service details must be confirmed in the project proposal.
Content reviewed:
NEXT PURCHASING ACTION
Start with the current-state evidence.
Enter machine ratings and your operating assumption, then add stop and interface observations.