
Bottled water production: solve one problem
Cap Feeder Jams and Missing Caps: Find the First Interrupted Handoff
A bottle leaving without a cap does not prove the hopper is too small or the capper is too slow. The closure may stop before orientation, be damaged during delivery, fail to transfer at pickup, or be present but incorrectly classified by inspection.
Keep the approved closure revision and trace identified caps through storage, orientation, delivery and pickup. Record the first missing or damaged closure and distinguish actual uncapped bottles from an inspection or counter disagreement. Quality must control suspect product.
Define a closure shortage before changing capacity
Freeze the cap drawing, neck finish, tamper-evident or tether geometry, material lot and actual feeder/capper configuration. Keep sample closures from before feeding and after the first suspect handoff. A carton label with the same nominal cap diameter does not establish equivalent geometry or compatibility.
Use one time window with matched bottle and cap observations. Record hopper refill, orientation outlet, delivery chute, pickup and inspection decisions from approved observation positions. A downstream low-cap alarm may be the consequence of an earlier obstruction; its timestamp is not automatically the initiating event.
Illustration only: 6 interruptions during a 30-minute record and 12 physically uncapped bottles among 600 inspected bottles describe different units. The uncapped-bottle fraction is 2%. It is not a feeder efficiency, an allowed defect rate or Allot Tech performance. Keep event counts, affected bottles and rejected closures separate.
Compare the cap at successive delivery boundaries
Observe stable running, refill transitions and restart separately. Preserve location and orientation with each sample; mixing rejected caps from the whole shift can erase where damage first appeared.
| Observed pattern | Evidence to retain | Scope to review |
|---|---|---|
| Storage contains caps but orientation outlet is starved | Approved cap lot, refill history and first interrupted point | Storage-to-orientation delivery, not automatically a faster capper |
| Caps are correct upstream but lodged or damaged after one handoff | Matched upstream/downstream samples and installed part identities | Serial-specific cap path, transfer and permitted format components |
| Delivery is present but the bottle has no applied cap | Linked pickup and bottle samples with machine phase | Pickup/application interface, not assumed hopper capacity |
| Physical closure is present but inspection reports missing | Independent approved reference and inspection/reject event | Inspection task and challenge method, separate from actual shortage |
Retest one approved closure-path correction
This is not a jam-clearing procedure. Qualified personnel must isolate stored energy, follow guarding and hygiene requirements and use OEM instructions. Do not reach into the sorter, force caps down a chute, alter air settings or bypass missing-cap rejection to keep output running.
- 01
Retain original parts, settings, approved cap/neck revisions, identified samples and the initiating-event log.
- 02
Agree a safe observation and quality-disposition method; compare stable, refill and restart phases using the same materials.
- 03
Have the responsible specialist review the first interrupted boundary and authorize one permitted correction after safe isolation.
- 04
Repeat the connected feeder-to-closed-bottle test, recording damaged caps, uncapped bottles and any supplied inspection/rejection separately.
- 05
Quality reviews sealing, tamper features and segregated product before acceptance; restored cap flow alone does not prove an acceptable closure.
Separate feeder, delivery and application supply scope
A feeder replacement will not by itself resolve a pickup mismatch, and a capper replacement does not establish why closures stopped upstream. Define the failed boundary before comparing offers. Include refill access, cleaning, retained delivery sections, format parts and restart responsibility in the scope review.
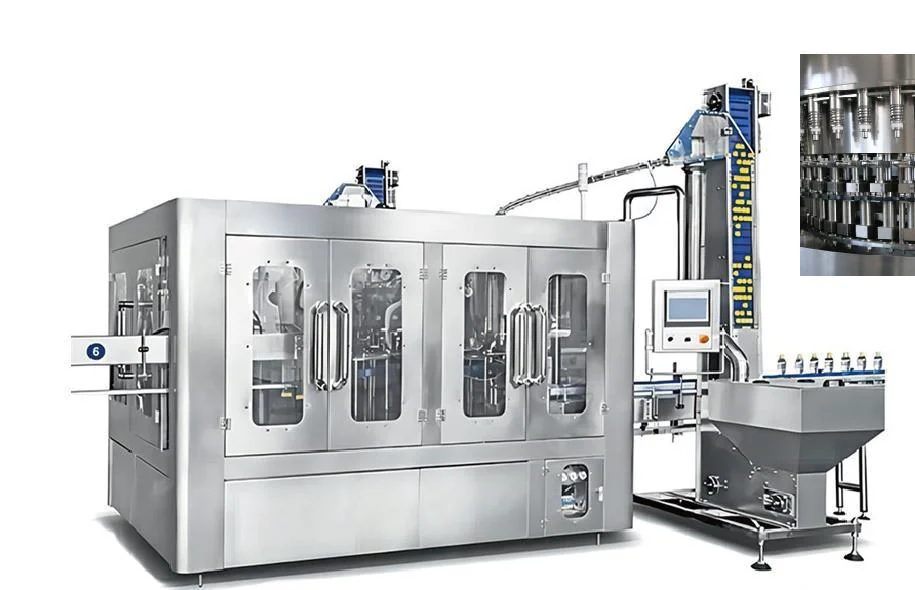
Send Allot Tech the actual closure and neck revisions, machine serials and linked evidence. Request written confirmation of compatible samples, orientation/delivery functions, change parts, utilities, inspection if supplied and connected acceptance. Do not infer a closure range, buffer size or guaranteed feed rate from the representative photograph.
Where a retained chute or an existing capper belongs to another supplier, assign who verifies its interface and who signs the connected trial. Mark unconfirmed geometry and responsibility as open items, rather than hiding them inside a claim that the feeder is compatible.
- Machine serials and cap-path layout
- Approved cap/neck drawings, lots and samples
- Installed orientation, delivery and pickup parts
- Matched cap/bottle samples at timed checkpoints
- Stable, refill and restart event records
- Quality disposition, retained interfaces and acceptance owners
Questions buyers ask
Does a full hopper rule out a cap-supply problem?
No. Storage inventory does not prove successful orientation, delivery or pickup. Trace the first interrupted handoff with the actual approved closure and matched observations.
Can missing-cap rejects be used as a feeder defect count?
Not without confirming the physical bottle and counting basis. Separate actual uncapped bottles, damaged closures, inspection classifications and repeated alarms from the same event.
Related troubleshooting guides
Water filling machine low output
Water filling machine low output →Water bottle shrink-pack problems
Water bottle shrink-pack problems →Cap leaks after capping
Cap leaks after capping →Wrinkled or skewed bottle labels
Wrinkled or skewed bottle labels →Uneven fill levels and underfill
Uneven fill levels and underfill →Conveyor jams and tipping
Conveyor jams and tipping →Missing or unreadable date codes
Missing or unreadable date codes →Wet bottles after drying
Wet bottles after drying →Startup rejects after changeover
Startup rejects after changeover →Missing or extra bottles in packs
Missing or extra bottles in packs →PET bottle scuffing and scratches
PET bottle scuffing and scratches →Label web breaks and torn liners
Label web breaks and torn liners →Cartons reopening after sealing
Cartons reopening after sealing →PET bottle bases rocking after blowing
PET bottle bases rocking after blowing →Filling valves dripping between bottles
Filling valves dripping between bottles →Reject signal without physical bottle removal
Reject signal without physical bottle removal →Water pallet loads leaning after stacking
Water pallet loads leaning after stacking →Ask Allot Tech to review the evidence
Send your machine identification, package drawing and timed observations. State what is unknown so the proposed scope follows the actual problem.