
Bottled water production: solve one problem
Bottle Label Web Breaks: Trace the First Rupture, Not Just the Last Stop
A stopped labeler and a loose strip of material do not identify the original break. Roll-fed OPP film, a pressure-sensitive release liner and tubular sleeve stock have different paths. Their normal cutting or peeling actions must not be mistaken for an uncontrolled web rupture.
Identify the actual labeling method, approved reel construction and first torn section. Keep reel-edge, splice and restart evidence linked to the same event. Separate a failed material web from label placement, code readability and a later application reject.
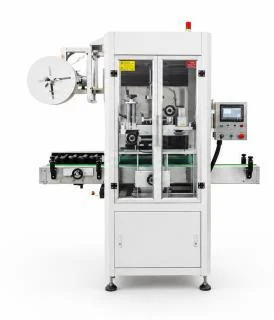
Identify the material that actually broke
Record labeler serial, method, job revision and approved material specification. State whether the failed strip is film, label face stock, release liner or tubular sleeve. Keep reel identity, winding direction, width, core and splice construction where specified; nominal label artwork alone does not establish material equivalence.
Retain the first damaged edge or torn section using approved safe handling, plus its location in the web path. Record reel start, reel change, splice, stop and restart separately. A downstream cutoff may be an intended machine action, and a strip found at rewind may have been damaged earlier.
Illustration: 4 unplanned ruptures across 8 comparable reels equal 0.5 rupture per reel. This comparison requires the agreed reel-length basis; keep processed length and splice count as separate records when reels differ. The example is not a machine performance result, an accepted break rate or a bottle-output measure.
Connect each break to its earliest evidence
Use approved observation from outside guards. An alarm list can help align timing but does not prove that the last indicated roller, cutter or sensor caused the initiating damage.
| Pattern | Evidence | Review boundary |
|---|---|---|
| Edge or reel damage visible before entering the machine | Retained incoming reel, lot, edge and handling record | Incoming material and permitted reel handling |
| Rupture follows the same splice or reel-change event | Linked splice construction, job and event position | Approved splice compatibility and change sequence |
| First damage appears after one web-path boundary | Safe upstream/downstream evidence and installed component IDs | Serial-specific path and permitted guide/drive/cutting review |
| No web rupture; labels are misplaced or rejected | Physical web reference and actual application/inspection result | Placement or inspection task, not automatically a web-break fault |
Repeat a controlled material and event comparison
This article supplies no tension, brake, nip, blade, heat or adhesive setting. Qualified personnel must follow isolation, cutting-edge, stored-energy and OEM precautions. Do not rethread moving machinery, bypass guards or hold the web by hand to suppress a break.
- 01
Preserve the approved reel/job version, original path and settings, retained torn material and event ledger.
- 02
Agree true-rupture criteria and a comparable processed-length, reel and splice basis for the actual labeling method.
- 03
Have qualified personnel examine the first damaged boundary after safe isolation and authorize one permitted correction.
- 04
Retest the same material route through agreed stable running, reel/splice change and restart events; record all ruptures.
- 05
Review web continuity together with label placement, application quality, rejection and material segregation before acceptance.
Specify the reel path and event responsibility
Damaged incoming reels, an incompatible splice and a problem at one installed path boundary require different evidence and work scopes. A higher-speed labeling station or an unconfirmed automatic splice option is not a demonstrated cure. Separate the web-continuity requirement from decoration quality.
Send Allot Tech approved material construction, representative reels and event-linked samples. Request written limits for the material route, retained modules, reel/core handling, splice if included, format parts, controls responsibility and connected acceptance. Do not treat sleeve, OPP and release-liner systems as interchangeable.
If the comparison includes a different supplier's reel or revised substrate, record it as a separate qualification condition. Preserve who approved the material and what remains unconfirmed. A smooth short run without a reel change does not qualify the change event that originally failed.
- Labeler serial, method and web-path layout
- Approved substrate, reel/core and job revisions
- Reel lots, winding and splice specifications where applicable
- Retained first-torn section and timed event location
- Processed length, reels, splices and restart records
- Application criteria, retained modules and acceptance owners
Questions buyers ask
Is every cut strip a label-web break?
No. Identify the actual method and distinguish intended cutting or liner peeling from uncontrolled rupture. Keep the first damaged section linked to its event and location.
Can one successful reel prove the splice and restart are qualified?
No. The acceptance trial must include the agreed reel-change, splice and restart cases using approved material. Stable running alone does not test those events.
Related troubleshooting guides
Water filling machine low output
Water filling machine low output →Water bottle shrink-pack problems
Water bottle shrink-pack problems →Cap leaks after capping
Cap leaks after capping →Wrinkled or skewed bottle labels
Wrinkled or skewed bottle labels →Uneven fill levels and underfill
Uneven fill levels and underfill →Conveyor jams and tipping
Conveyor jams and tipping →Missing or unreadable date codes
Missing or unreadable date codes →Wet bottles after drying
Wet bottles after drying →Startup rejects after changeover
Startup rejects after changeover →Missing or extra bottles in packs
Missing or extra bottles in packs →Cap feeder jams and missing caps
Cap feeder jams and missing caps →PET bottle scuffing and scratches
PET bottle scuffing and scratches →Cartons reopening after sealing
Cartons reopening after sealing →PET bottle bases rocking after blowing
PET bottle bases rocking after blowing →Filling valves dripping between bottles
Filling valves dripping between bottles →Reject signal without physical bottle removal
Reject signal without physical bottle removal →Water pallet loads leaning after stacking
Water pallet loads leaning after stacking →Ask Allot Tech to review the evidence
Send your machine identification, package drawing and timed observations. State what is unknown so the proposed scope follows the actual problem.